A production-ready PCB layout is not merely a routing task completed once all nets are connected. It is the convergence point where the schematic, components, stackup, mechanical constraints, test strategy, and selected manufacturing technology are fully aligned, ensuring the board can be fabricated and function as specified—well beyond the laboratory environment.
For complex products, this distinction is critical. An overlooked return path, ambiguous impedance tolerances, or a footprint with marginal solder process windows can lead to EMC issues, instability, or yield loss that only surface after an expensive prototyping iteration. Therefore, manufacturing readiness must be engineered into the layout from day one, rather than verified as an administrative afterthought.
What Defines a Production-Ready PCB Layout?
A layout is production-ready when the fabricator can build the board without ambiguity, the assembly provider can place and solder components within a realistic process window, and the engineering team has comprehensive documentation to verify the end result. Simultaneously, the layout must fulfill all electrical requirements: signal integrity, power integrity, EMC, isolation, thermal management, and mechanical tolerances.
This demands more than simply adhering to design rules. A DRC-clean routing only proves that the layout satisfies the parameters entered into the CAD system. If these constraints fail to account for fabricator capabilities, material selections, creepage and clearance distances, HDI sequences, or critical interfaces, a formally error-free design may still prove challenging or prohibitively expensive to manufacture.
In practice, the objective is to eliminate ambiguity. Every critical design decision must be justified and verifiable: Which impedance profile must be met? Which laminate characteristics apply at the relevant operating frequency? Is the via structure viable within the specified buildup? Can the BGA packages be reliably inspected? And is there adequate copper balancing and thermal via density to maintain components within operational temperature limits?
Stackup Is an Electrical Specification
Stackup definition is frequently deferred because it is mistakenly treated as a mere manufacturing detail. For high-speed, RF, and dense digital designs, this approach is fundamentally flawed. The layer stackup dictates reference planes, coupling between signal and power planes, return current distribution, impedance control, attenuation, and breakout routing capabilities for fine-pitch components.
A 100-ohm differential pair is not just a trace-width design rule. It is governed by trace cross-section geometry, post-etch copper thickness, dielectric properties, reference plane proximity, and manufacturing tolerances. At higher data rates, insertion loss, via stubs, mode conversion, and layer transitions must be analyzed as a comprehensive transmission channel. An off-the-shelf, standard stackup may suffice for a moderate industrial bus, but it falls short for high-speed SerDes links or RF circuits with stringent loss budgets.
Power and ground planes require the same rigorous planning. A PDN exhibiting excessive loop inductance between decoupling capacitors and power pins will induce transient voltage noise, regardless of proper regulator sizing. Component placement, via structures, interplane capacitance, and return paths are explicit layout decisions—not post-layout optimizations.
Return Paths and Layer Transitions Must Be Explicit in the Design
High-speed signals do not intuitively take the shortest physical path. High-frequency return currents travel directly beneath the signal trace within the nearest adjacent reference plane. When a signal transitions between layers, its return path must transition accordingly. Lacking appropriate stitching vias or AC-coupling return paths between reference planes introduces impedance discontinuities, escalating electromagnetic emissions, jitter, and susceptibility to noise.
The same considerations apply to split planes. While split planes may be necessary, high-speed traces must never cross a split without a defined return path control strategy. This remains a classic failure mode, as a layout can appear clean on the screen while harboring fundamental EMC vulnerabilities.
Design for Manufacturing Begins at the Footprint
A footprint must be optimized electrically, mechanically, and from a process standpoint. While the recommended land pattern in a component datasheet serves as an initial guideline, it is rarely the optimal production solution. Solder paste volume, component tolerances, panelization, surface finishes, soldering methodology, and manufacturing process windows all dictate proper pad geometry.
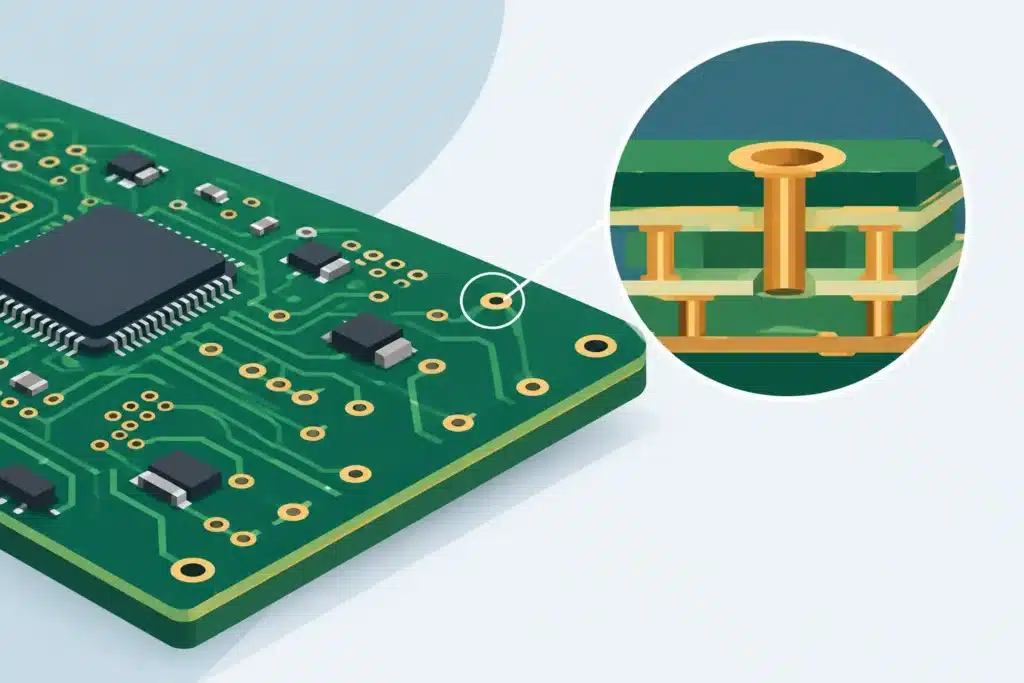
For BGAs and fine-pitch components, breakout routing, via-in-pad technology, via filling and capping, as well as solder joint inspectability must be resolved early. While routing around compromised footprints is often technically possible, it frequently incurs significant costs: additional layers, costly HDI builds, or reduced manufacturing yields. The optimal strategy balances production volume, real estate, reliability requirements, and component package specifics.
Component placement must equally support assembly and testing. Maintain adequate component clearances to facilitate rework, avoid shadowing critical test points with tall components, and enforce consistent polarization orientation. For sensitive analog and RF circuitry, physical isolation, localized shielding, and controlled ground strategies invariably yield far better performance than retroactive filtering applied to mitigate suboptimal layout geometry.
EMC and Thermal Management Cannot Be Deferred
EMC performance is the cumulative result of current loops, loop areas, edge rates, cabling, enclosure dynamics, and board layout. A printed circuit board utilizing high-speed switch-mode regulators or fast digital transitions can easily fail radiated emissions compliance, even if functional testing on the lab bench succeeds. Therefore, noise sources, coupling paths, and susceptible circuits must be rigorously identified before layout freeze.
Critical design areas typically encompass the switch node of DC/DC converters, clock distribution networks, connector interfaces, common-mode return paths, and the partitioning between digital and analog domains. Minimize high di/dt loop areas, preserve reference plane continuity, and place decoupling networks according to actual current flow rather than schematic topology.
Thermal design demands equal discipline. Copper pours beneath high-power components assist dissipation, but provide marginal benefit without low-resistance thermal conduction paths to internal or opposite copper layers. Thermal vias, finished copper thickness, system airflow, chassis heatsinking, and mutual component heating must be evaluated comprehensively. A component operating marginally within its rating at 23 °C ambient may quickly exceed maximum junction temperatures within a sealed industrial enclosure.
Documentation Must Eliminate Manufacturing Ambiguity
Gerber or ODB++ datasets do not constitute complete manufacturing documentation on their own. The fabricator must clearly interpret base material specifications, stackup construction, copper weights, controlled impedance profiles, drill schedules, specialty via requirements, surface finishes, general tolerances, and applicable IPC class standards without guesswork.
Similarly, assembly datasets must be fully aligned with the Bill of Materials (BOM), centroid/placement files, reference designators, revision controls, and assembly drawings. When alternate components are approved, their footprints, package heights, polarities, and thermal characteristics must be verified. A component substitution deemed simple by procurement can severely impact reflow profiles, mechanical clearances, or high-frequency circuit behavior.
For high-reliability systems, documentation must clearly define acceptance criteria for critical metrics: impedance coupon testing, microsectioning, via fill quality, solder joint inspection, automated optical/X-ray inspection, and non-conformance handling. This is paramount for IPC Class 2 and Class 3 applications, where full traceability and repeatable quality are contractual imperatives.
A Design Review Must Uncover Root Causes, Not Just Rule Violations
An effective PCB design review evaluates the coherence between project requirements and physical implementation. Merely checking mechanical clearances, silkscreen legibility, and unrouted nets is insufficient. The review must critically challenge decisions carrying the highest operational and financial risks.
The following four domains should be explicitly audited in any comprehensive review:
- Electrically critical nets: impedance control, length/delay matching, reference plane continuity, termination schemes, via transitions, and return paths.
- PDN and EMC: decoupling placement, power plane topology, high di/dt noise loops, connector interfaces, and chassis ground bonding.
- Fabrication and assembly: footprint geometry, panelization schemes, manufacturing limits, soldering processes, inspection access, and reworkability.
- Mechanical and test integration: 3D envelope clearances, mounting and hardware, thermal management paths, test point coverage, in-circuit programming, and cable routing.
The fidelity of a review depends directly on the clarity of the underlying inputs. If specifications regarding operating frequency, environmental conditions, target operational life, emission profiles, and production volumes are undefined, they must be highlighted as explicit technical risks. A design cannot be verified against criteria that exist solely as assumptions.
When to Engage a PCB Specialist
The earlier critical architectural choices are made, the fewer redesign iterations are required. This does not imply that an external specialist must handle the entire project lifecycle. Some development teams need an early-stage stackup and design rule review; others require complex routing from a finalized schematic; still others face a failing EMC test or yield fallout during pilot production.
In high-complexity designs, direct engagement with an experienced PCB specialist yields significant technical value. Signal integrity, HDI, RF, power distribution networks, and manufacturability constraints continuously interact; failures frequently originate at the interfaces between these engineering domains. Wise Choice Support bridges these technical interfaces from initial design specifications through to released manufacturing datasets, ensuring engineering integrity remains uncompromising.
A logical next step is reviewing the three decisions that carry the highest cost penalty if altered late: stackup definition, critical footprint/via architectures, and test/assembly access. Addressing these before locking the layout significantly maximizes the likelihood that your initial production run serves as a swift design verification rather than an expensive troubleshooting exercise.