A PCB can look correct on screen and still fail when exposed to switching currents, fast edge rates, temperature variations, and an actual manufacturing line. Therefore, a PCB design review checklist must not be merely a quick visual inspection prior to release. It must systematically verify whether the schematic, stackup, component placement, routing, and fabrication data truly support the intended functionality for which the product was engineered.
This applies particularly to telecommunications, radar, medical technology, industrial, defense, and data center equipment. In these domains, an unbroken return path, an incorrect via transition, or inadequate copper balancing does not necessarily surface during initial bench testing. The failure may only manifest later as EMC non-compliance, temperature-dependent instability, degraded yield, or a costly board respin.
Begin the Review with the Design Baseline
A layout cannot be evaluated in isolation from its requirements. Prior to reviewing traces, vias, and polygons, the review must establish the electrical, mechanical, and manufacturing prerequisites. Are interface data rates, voltage levels, impedance targets, and EMC objectives formally documented? Have environmental requirements, IPC class, operational lifespan, vibrational loads, and test coverage requirements been defined?
Many issues stem from making assumptions regarding these parameters rather than establishing definitive specifications. For instance, a 50-ohm RF trace is not solely a characteristic of trace geometry. It is governed by stackup, dielectric thickness, copper weight, solder mask, and the capabilities of the target fabrication facility. Similarly, differential impedance depends not only on trace width, but also on intra-pair spacing, reference plane continuity, and laminate manufacturing tolerances.
The review should also determine whether requirements remain consistent across the product lifecycle. A prototype board, a low-volume product, and a mission-critical system can have vastly different demands regarding material selection, component derating, test coverage, and documentation. This is where design decisions must align with real-world operational demands rather than relying on default CAD tool configurations.
PCB Design Review Checklist for Stackup and Return Current Paths
The stackup serves as the foundation for signal integrity, power integrity, and EMC. If finalized late in the design cycle, routing inevitably results in compromises that cannot be remedied by subsequent design rules.
First, verify that each signal layer has an adjacent, continuous reference plane. High-speed signals and clock traces must be able to return current directly beneath or above the trace. Crossing a split in the ground plane, a board cutout, or an area lacking a continuous reference forces the return current into an extended loop. This amplifies noise, radiated emissions, and susceptibility to external interference.
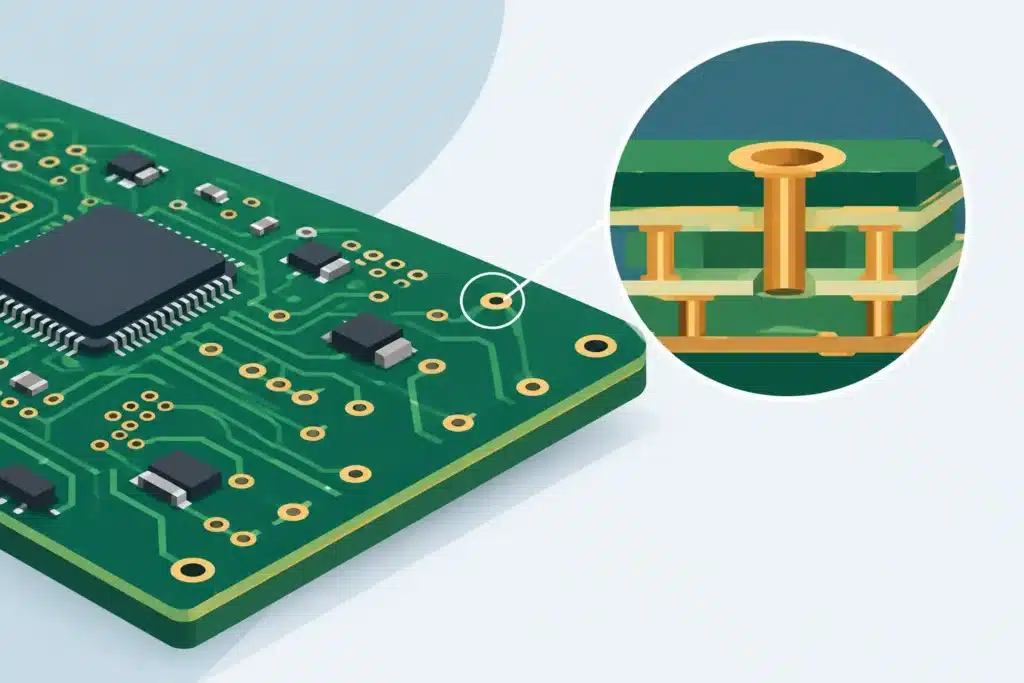
Via transitions demand equal scrutiny. When a signal transitions from one layer to another, the return current requires a controlled path between the corresponding reference planes. For signals transitioning between ground-referenced layers, an adjacent ground return via placed close to the signal via may be mandatory. When transitioning between distinct reference potentials, stitching capacitor placement and frequency response must be engineered rather than added as an afterthought.
Furthermore, review whether the stackup is manufacturable by the selected PCB fabricator. Controlled impedance must be based on the fabricator's exact material buildup and process tolerances, not a generic template. For multi-gigabit channels, RF, high-speed ADC/DAC interfaces, and DDR memory, dielectric loss, dispersion, stubs, and skew must be factored into the assessment. A via structure that is electrically acceptable at 100 MHz can easily become the dominant failure mechanism at several gigabits per second.
Signal Integrity: Evaluating the Complete Interconnect
Verifying that a trace meets nominal width requirements is rarely sufficient. A critical interconnect encompasses the driver, package pads, vias, trace geometry, connectors, receiver, and all transitions in between. The review must identify nets exhibiting fast edge rates, even if nominal clock frequencies appear low. Edge rate energy—rise and fall time—dictates when an interconnect must be treated as a transmission line.
For each critical single-ended or differential interconnect, the review must verify characteristic impedance, route length, timing skew, via count, reference plane changes, and termination topology. Differential pairs do not merely require length matching; they must be routed as a cohesive electromagnetic pair maintaining consistent geometry, identical via structures, and minimal phase distortion. Unnecessary serpentine routing to satisfy tight length tolerances can degrade signal quality if applied without considering mutual coupling and local impedance discontinuities.
Vias stubs warrant dedicated inspection. Test pads, T-junctions, through-hole via stubs, and component branches can generate reflections that only become problematic across specific temperature ranges, cable lengths, or operating loads. Backdrilling, blind vias, or topology modifications may be required, provided that frequency content, production budget, and fab capabilities justify their implementation.
PDN and Decoupling Must Be Evaluated as a System
Power delivery network instability cannot be remedied by simply scattering capacitors arbitrarily around an IC. A rigorous design review evaluates the PDN holistically from the voltage regulator module to the load: transient current profiles, allowable voltage ripple, plane impedance, via loop inductance, capacitor ESR and ESL, and physical placement.
Begin with circuits that exhibit high or fast dynamic current transients, such as FPGAs, processors, RF power amplifiers, motor drivers, and switch-mode regulators. Are the power and ground planes placed closely adjacent to provide low planar inductance? Are decoupling capacitors positioned such that the loop inductance from the power pin through the capacitor to the ground plane is minimized? A capacitor placed on the same electrical net is ineffective if its routing vias and location introduce an overly inductive path.
Review current carrying capacity and thermal dissipation. Narrow necking in copper pours, inadequate via quantities at regulator outputs, or insufficient copper weight cause voltage drops and localized thermal stress. For high-current designs, DC drop analysis and thermal simulation should validate visual checks. Layer count, copper weight, board dimensions, and long-term reliability must be carefully balanced.
EMC Must Be Engineered into the Component Placement
EMC cannot be resolved simply by adding shielding cans and ferrite beads following initial pre-compliance testing. Component placement establishes early on whether noise sources, sensitive analog circuits, and external interfaces can be maintained under control.
Switching converters must feature compact high-di/dt current loops and remain physically isolated from sensitive analog circuits, RF front-ends, and precision reference voltages. Input and output networks of a regulator must not overlap, preventing high-frequency noise from coupling back into input rails. Clock generators, oscillators, and high-speed parallel buses must be placed with a clear understanding of their return paths and spatial separation from I/O connectors, antennas, and cable entry points.
On external interfaces, ESD and transient protection devices must be placed directly at the connector interface before transients propagate across the board. The return path from the protection device to chassis ground or system GND is just as critical as the component selection itself. A TVS diode routed with an inductive, high-impedance ground connection will underperform significantly compared to its datasheet specifications.
Fabrication, Assembly, and Test Are Integral to the Design
A design is not production-ready merely because Gerber or ODB++ files can be generated without errors. The review must verify whether the PCB fabricator can reliably manufacture the board and whether assembly processes yield consistent, repeatable results.
This includes parameters such as annular ring width, drill diameters, aspect ratios, solder mask slivers, copper-to-edge clearances, fine-pitch footprints, via-in-pad requirements, panelization schemes, and impedance tolerance requirements. HDI solutions utilizing microvias and sequential lamination may be necessary, but their use must be deliberate. While they provide routing density on tightly packed designs, they also elevate manufacturing cost, lead times, and vendor qualification requirements.
Validate DFM rules directly against the chosen manufacturer's process capabilities rather than generic industry minimums. A feature that can theoretically be produced is not necessarily one that yields stably in volume production. Furthermore, IPC Class 2 and IPC Class 3 mandate fundamentally different criteria regarding trace spacing, annular rings, solder joint criteria, and documentation.
Design for Test (DFT) must be thoroughly assessed prior to layout sign-off. Is there physical access to critical power rails, reset lines, programming headers, boundary scan chains, and low-level digital interfaces? Can automated test fixtures access test points without interfering with mechanical enclosures, heatsinks, or shields? During production troubleshooting, a properly architected test strategy is often the difference between a minor containment issue and an expensive diagnostic effort.
Ensure the Review is Traceable and Actionable
An effective engineering review does not deliver a disjointed list of observations. Every finding must be categorized by risk level, clear mitigation action, ownership, and formal sign-off. It is vital to distinguish between critical failure risks, parameters requiring further simulation or validation, and low-priority aesthetic improvements. Otherwise, critical return-path design flaws risk being obscured by cosmetic layout comments.
For complex, high-reliability designs, the review should be conducted in distinct phases: first architecture and stackup, followed by component placement and critical routing, and finally fabrication data, assembly, and testability. This phased approach mitigates the risk of uncovering fundamental architecture flaws when layout changes become prohibitively expensive. At Wise Choice Support, reviews focus on the underlying physical mechanisms of the design—not merely on whether the layout clears automated CAD DRC checks.
The most cost-effective bug is the one caught prior to fabrication. Leverage the design review to lock down critical technical decisions while modifications remain straightforward, preventing unverified assumptions from driving up hardware costs.