A differential signal rarely fails simply because two traces lack identical physical lengths. It more frequently fails because the pair loses its reference plane, transitions through an unoptimized via, or is sized according to generic rules rather than the actual PCB stackup. Consequently, this guide to differential pair routing focuses on the parameters that govern signal integrity, EMC, and manufacturability in production-grade PCB designs.
Guide to Differential Pair Routing in Real-World PCB Stackups
Differential pair routing must be approached as a transmission line problem, not merely as a CAD layout exercise. The objective is not just to route P and N parallel to each other. The objective is to achieve the specified differential impedance, maintain the continuity of the return path, and confine total timing skew within the interface budget.
This begins with a precise definition of the interface. Does the design implement USB, Ethernet, LVDS, PCIe, SerDes, CAN FD, or a proprietary high-speed link? The constraints governing impedance, loss, common-mode noise, and skew vary substantially. While a 100-ohm differential pair is common, it is not universal. Certain interfaces require 85 ohms, 90 ohms, or a value defined by the component and connector models.
The nominal impedance stated in a datasheet is merely a starting point. The physical geometry must be calculated based on the specific stackup the PCB manufacturer can reliably produce. Trace width, trace separation, dielectric height above the reference plane, dielectric constant (Dk), copper thickness, and solder mask influence all dictate the final value. If a single dielectric layer in the stackup is modified late in the design cycle, the routing constraints must be updated accordingly.
Differential Impedance Is a System-Level Requirement
A differential pair consists of two single-ended conductors characterized by self-impedance as well as mutual coupling. As the traces are routed closer together, coupling increases and differential impedance generally decreases. As separation increases, each trace behaves more like an independent, single-ended transmission line.
There is no universal rule dictating that spacing must always equal three times or five times the trace width. While such rules of thumb can serve as crude guidelines for isolating adjacent signals, they do not replace rigorous calculation. In high-density interconnect (HDI) designs, trace geometry may be constrained by laser vias, BGA pitch, and laminate construction. In RF or ultra-high-speed digital layouts, dielectric loss and dispersion are often far more critical than trace area alone.
Therefore, define routing rules using explicit manufacturing parameters: target differential impedance, tolerance, trace width, spacing, copper weight, layer assignment, and reference plane. If the PCB fabricator alters prepreg thickness or copper distribution, the consequences must be assessed prior to production—not after a post-fabrication TDR measurement on assembled boards.
Prioritize Return Paths over Length Matching
In differential transmission, a significant portion of the electromagnetic field is contained between the two traces. However, this does not render the reference plane insignificant. Asymmetries, mode conversion, vias, component pads, and parasitic coupling to surrounding structures inevitably drive return currents into the plane. An uninterrupted reference plane in close proximity to the signal layer minimizes both radiated emissions and noise susceptibility.
Never route differential pairs across ground splits, cutouts, slots, or fragmented planes. When changing layers, provide a continuous reference for the pair on the destination layer. If the return current must transition between two ground planes, place dedicated ground stitching vias adjacent to the signal vias. If the reference shifts between ground and a power plane, the path becomes significantly more sensitive and must be evaluated against the PDN topology and local decoupling effectiveness.
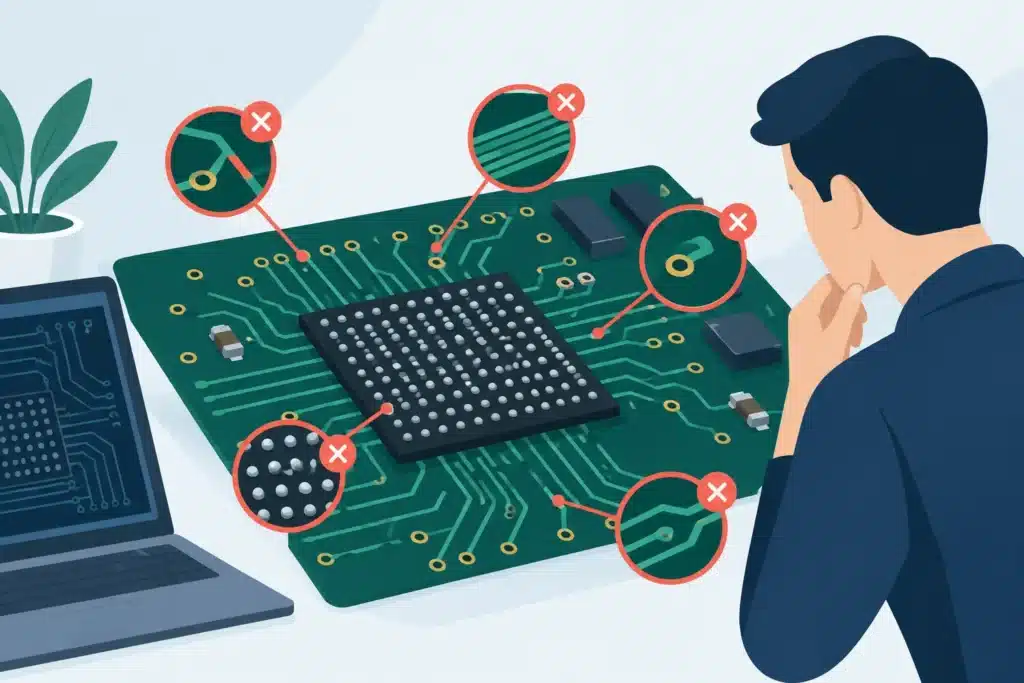
A visually neat, parallel routing implementation can still be electrically flawed. This frequently occurs during BGA breakout—where traces are forced across plane voids—or at connector interfaces where footprints lack an engineered return path.
Via Transitions Must Be Designed as Transmission Lines
Every via introduces parasitic inductance, capacitance, and often an open stub. At lower data rates, these effects may be negligible. At fast edge rates and multi-gigabit speeds, an unused plated through-hole stub can trigger severe reflections and resonances that close the eye diagram.
Minimize layer transitions, but not as an absolute dictate. A short, controlled transition to an optimal reference layer can be preferable to a long trace route on a compromised layer. When vias are unavoidable, enforce symmetrical geometry, identical via counts, and matched parasitics across both P and N lines. Via pad diameter, antipad geometry, drill size, stub length, and stitching via placement must all be factored into the design.
Backdrilling is required whenever the electrical length of the remaining through-hole stub becomes significant relative to the signal’s frequency content. However, this imposes tighter tolerances, additional verification, and increased fabrication costs. In HDI stacks, blind and buried vias can provide a superior alternative, though via transition impedance and fabricator capabilities must still be fully validated.
Length Matching: Prioritize What Actually Matters
Intra-pair skew represents the propagation time difference between the P and N conductors. Excessive skew converts differential signals into common-mode noise, degrades receiver margins, and increases EMI. However, acceptable skew limits are dictated by the interface specification, not by arbitrary CAD defaults.
Permissible length delta depends on signal rise and fall times, dielectric velocity, driver tolerances, receiver common-mode rejection, and overall channel timing margins. Package and pin delays inside BGAs, connectors, and cables frequently exceed the delta introduced by short PCB traces. Consequently, length matching must be evaluated across the complete channel from transmitter die to receiver die, rather than solely on the PCB layout.
Serpentine tuning resolves mathematical length discrepancies only when implemented properly. Tightly spaced, parallel segments within a meander couple to one another, altering effective propagation velocity. As a result, a visually matched trace can still exhibit significant electrical skew. It is far better to implement loose, open tuning segments with adequate clearance between parallel sections, positioned exclusively over solid reference planes.
Topological symmetry is equally critical. If one trace detours around a component while the other routes near a plane void or an aggressive signal, the physical lengths may match, but the electrical environments do not. True symmetry applies to the entire transmission path.
Spacing, Coupling, and EMC Without Generic Formulas
A differential pair requires controlled internal coupling without unintended coupling to adjacent nets. Spacing from clocks, high-di/dt switching nodes, switch-mode inductors, memory buses, and adjacent high-speed pairs must be established based on stackup construction, layer assignment, and the energy of nearby noise sources. Clearance that provides sufficient isolation on an internal stripline layer may prove inadequate on an external microstrip layer.
Isolate high-speed pairs from noisy switching nodes and the perimeter of reference planes. Eliminate redundant test pads, asymmetrical teardrops, and mismatched solder mask openings on sensitive nets. These physical discontinuities introduce common-mode imbalance between P and N, especially near transmitters, receivers, and AC-coupling capacitors.
When using AC-coupling capacitors, maintain symmetrical component placement and routing. The layout must not introduce trace stubs or force the pair through asymmetric pad geometries. Similarly, common-mode chokes must be selected and routed with an understanding of both differential and common-mode behavior. While they improve EMC performance, inappropriate footprints or unbalanced traces can introduce severe signal integrity penalties.
From CAD Rules to Production-Ready Layout
A reliable PCB design constraint set must govern more than basic trace widths and clearances. It should also control layer assignments, valid reference planes, maximum via stub lengths, tuning regions, aggressor clearances, and breakout rules for BGAs and connectors. These constraints must correlate directly to the stackup and interface specifications, ensuring that design reviews do not rely on subjective judgment or individual habit.
Prior to sign-off, differential nets should be evaluated across three stages. First, verify trace geometries against the stackup and target impedance profiles. Second, audit the physical routing for plane splits, asymmetries, via stubs, and component transitions. Finally, evaluate the complete channel using appropriate modeling or full-wave simulation whenever data rates, trace lengths, or application risks warrant it.
In mission-critical electronics, comprehensive documentation is an intrinsic part of the design. Fabrication drawings, stackup details, impedance tables, tolerance budgets, and test coupon specifications must be aligned. At Wise Choice Support, bridging the gap between signal integrity, layout rigor, and the fabricator's true process capabilities is precisely what ensures a design is fully production-ready, rather than merely ready for Gerber export.
The optimal time to correct an impedance discontinuity or poor differential transition is before the layout is frozen. Finalize the stackup, component footprints, return paths, and channel loss budget early, enabling fully justified routing decisions and ensuring the finished PCB delivers the high-speed performance your mission-critical system demands.