A signal integrity failure example often begins with a measurement that appears acceptable in the laboratory, but fails under temperature variations, cable discrepancies, or full system load. The product might communicate at a low data rate, but exhibits bit errors, overshoot, or EMC issues when interface speeds increase. The root cause is rarely a single defective component. Typically, it lies in the interaction between the stackup, reference planes, vias, termination, and the actual geometry of the PCB layout.
For engineering teams working with DDR, Ethernet, SerDes, LVDS, PCIe, USB, or high-speed ADC/DAC interfaces, this is a well-known risk. A trace is no longer merely a copper path between two pins; it is a transmission line and must be treated as such from the schematic to manufacturing data.
A concrete signal integrity failure example
Consider a PCB with a 1 Gbit/s differential interface between an FPGA and a PHY. The schematic is correct, the components are qualified, and the nominal impedance requirements are specified as 100 ohms differential. During bring-up, intermittent link drops occur. The issue manifests particularly during high activity on adjacent interfaces and proves difficult to reproduce consistently across all prototypes.
Measurements using an appropriate active probe reveal ringing at the receiver. The signal exhibits overshoot followed by reflections that take several nanoseconds to settle. The eye diagram is open under ideal conditions, but the margin collapses when power supply noise and temperature variations affect the system.
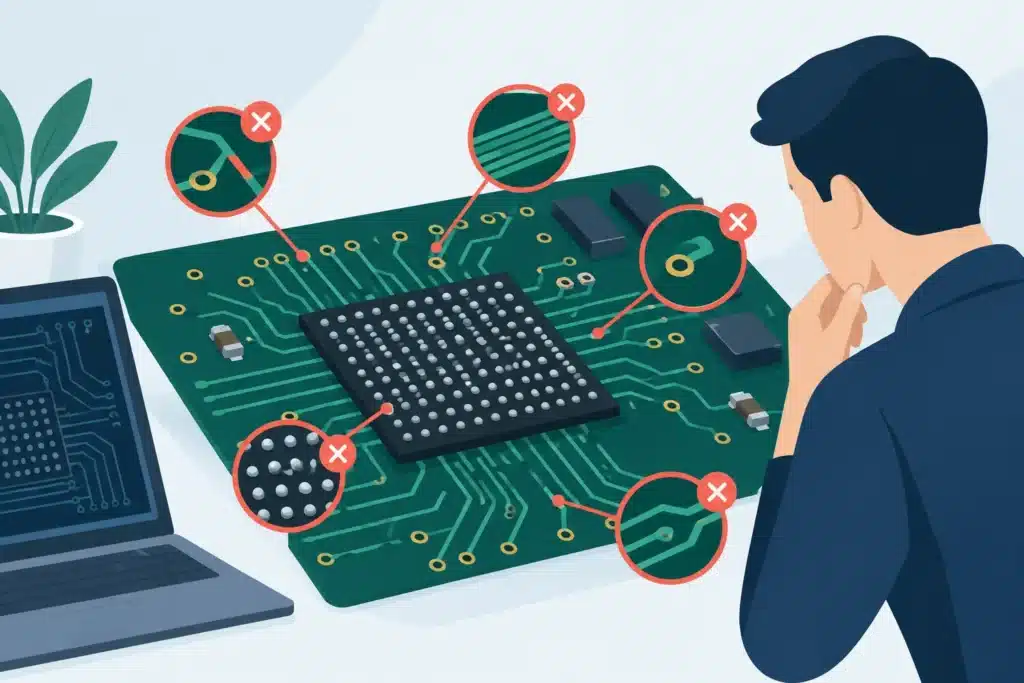
The initial explanation might suggest inadequate termination. In this case, however, the root cause is more specific: while the differential pair is routed correctly along the majority of its path, it traverses two layer transitions utilizing standard through-hole vias. The stub from the unused via layers creates a significant impedance discontinuity. Concurrently, the reference plane is discontinuous near a via pair because the signal changes layers without a continuous return path.
The result is two simultaneous failure mechanisms: the via stub induces resonance and reflections, while the compromised return path converts a portion of the differential energy into common-mode noise. This not only degrades signal quality, but also increases the likelihood of EMC emissions from the area surrounding the layer transition.
Why the defect is detected late
Many signal integrity defects arise because a layout is evaluated visually rather than electrically. A differential pair may appear pristine, featuring consistent spacing, parallel routing, and seemingly accurate length matching. However, if the local stackup changes, the reference plane is interrupted, or coupling to surrounding structures fluctuates, the electrical behavior is no longer controlled.
It is also a mistake to treat length matching as the sole criterion. For high-speed interfaces, the critical parameter is often propagation delay rather than physical length. Two traces of identical length can have differing propagation delays if routed on different layers, adjacent to different copper features, or subject to variations in effective dielectric constant along their paths.
In this example, the initial prototype board may function adequately in a short bench test setup. However, production tolerances in laminate Dk, lot-to-lot variations, and slightly altered cabling configurations will push the system beyond its actual operating margin. Consequently, a design should never be signed off solely because a single prototype powers up and communicates.
The return path is part of the signal
A high-speed signal always follows its return path. On a stripline trace, the return current flows primarily in the adjacent reference plane. When the signal encounters a split, a void in the plane, or a layer transition without appropriate stitching vias, the return current is forced onto a longer, uncontrolled loop.
This introduces local inductance, ground potential differences across reference domains, and radiated emissions. In differential interfaces, it is tempting to assume that the return current flows exclusively in the complementary trace. This is only partially true and depends heavily on the coupling factor of the pair. In the presence of asymmetry, suboptimal via geometry, or common-mode content, the reference plane remains critical.
Vias must be engineered, not merely placed
A standard via is not inherently suitable for high-speed signals. Its pad size, antipad, barrel diameter, stub length, and layer transition geometry are integral to the electrical model. At high data rates, backdrilling, blind/buried vias, or specialized via structures may be required to eliminate stub resonance and maintain impedance control.
This depends on the edge rate (rise/fall time) of the signal, not merely the nominal clock frequency. A 100 MHz clock with very steep edges can impose more stringent layout requirements than a lower-speed interface with a moderate rise time. Design rules should therefore be derived from actual signal energy and protocol margins rather than a single frequency figure in a block diagram.
Systematic root cause analysis
Effective troubleshooting begins by isolating whether the issue stems from the signal path, PDN, termination, stackup, or measurement methodology. Measurements taken using a passive probe with a long ground lead can introduce parasitic inductance, displaying ringing that does not exist in the circuit itself. For critical interfaces, probe selection, grounding point, and measurement bandwidth must be carefully evaluated.
Subsequently, the measurements must be correlated with the physical geometry of the layout. Where are the layer transitions, AC coupling capacitors, test points, splits, connectors, and component pads located? A TDR (Time-Domain Reflectometry) measurement can pinpoint where along the interconnect the impedance deviates, while S-parameter data and channel modeling quantify insertion loss, return loss, and crosstalk.
In practice, the review should cover at least the following four aspects:
- The actual stackup, including dielectric thicknesses, copper weights, and material properties provided by the PCB manufacturer.
- The impedance profile across traces, pads, vias, connectors, and any termination elements.
- The return path across every layer transition, decoupling/coupling capacitor, and plane clearance area.
- Coupling to potential aggressors, including clock lines, switch-mode power supplies, parallel buses, and connector interfaces.
Simulation does not replace physical measurement, and measurement does not replace fundamental design competence; both disciplines must be integrated. Pre-layout simulation confirms whether a topology provides adequate margin, while post-layout analysis verifies that the actual routing complies with specifications once vias, component placement, and mechanical constraints are factored in.
Corrective actions and trade-offs
In the highlighted example, the optimal corrective action often involves redesigning the layer transition. Backdrilling can eliminate the critical stub, but requires consultation with the fabricator regarding tolerances, residual stub limits, and process capabilities. Blind vias can provide a cleaner signal path, but increase HDI complexity and manufacturing costs. Frequently, the most robust solution is simply adjusting the component placement to eliminate the layer transition altogether.
Placing ground stitching vias adjacent to the signal vias ensures a low-inductance return path, but will not inherently resolve problems caused by stubs or incorrect antipad dimensions. Similarly, adjusting a termination value may mitigate reflections, but cannot resolve a fundamental discontinuity in channel geometry. Therefore, root causes must be addressed rather than merely treating the symptoms.
Manufacturing constraints must also be accounted for. An impedance specification on a drawing is of limited value if the stackup is not locked down, if the manufacturer can substitute materials without electrical verification, or if test coupons and tolerances are left undefined. For IPC Class 2 and particularly IPC Class 3 designs, signal integrity requirements must be tied to verifiable manufacturing data, not solely to a CAD layout ruleset.
Preventing defects before prototyping
The most cost-effective stage to resolve signal integrity issues is prior to finalizing routing. This requires interface requirements, stackup design, component placement, and PCB manufacturing technologies to be evaluated holistically. Consequently, a design review should not be confined to clearance and DRC checks; it must validate critical nets, the impedance environment, return paths, via strategies, PDN coupling, and EMC implications.
Wise Choice Support specializes in bridging this gap between high-speed layout, simulation, and production-ready documentation. The objective is not merely a board that can be manufactured, but a printed circuit board whose electrical integrity is maintained throughout prototyping, volume production, and mission-critical field operation.
When a signal integrity failure results in an expensive redesign cycle, it is frequently because critical details were treated as an afterthought. In complex PCBs, these details are fundamental to the physical architecture. The correct engineering decision is to analyze critical signal paths while there is still flexibility to optimize topology, stackup, and component placement.