A PCB can be electrically correct in the CAD system and still represent a poor manufacturing design. This occurs when tolerances, material selection, panelization, soldering processes, and test strategies are addressed only after the layout is released. This guide to design for manufacturing focuses on making production an active design parameter from the very first stackup—not merely a final check at the fabrication facility.
For complex products, DFM is not just a matter of observing generic minimum trace widths and clearances. It is the interplay between electrical requirements, PCB technology, assembly processes, test strategy, and expected production volume. A rule that applies to a simple four-layer industrial board can be fundamentally incorrect for an HDI design featuring fine-pitch BGAs, controlled impedance, and stringent operational reliability requirements.
What Design for Manufacturing Means in a PCB Project
Design for manufacturing, commonly abbreviated as DFM, is the systematic adaptation of board layout and manufacturing data to the processes that will ultimately fabricate and assemble the board. The objective is not simply to pass the first prototype through the line. The objective is a design that can be manufactured with predictable yield, consistent quality, and a clearly defined cost profile.
This requires involving the PCB fabricator and EMS partner early in the process. The fabricator's capabilities dictate, for example, the feasible minimum sizes for laser vias, annular rings, traces, clearances, and registration tolerances. Assembly capabilities determine the placement of component clearances, fiducials, solder paste, BGA escape routing, and through-hole components. If these factors are identified only upon Gerber or ODB++ release, the result is frequently a redesign, project delays, or costly specialized processes.
Furthermore, DFM must not be decoupled from signal integrity, power integrity, and EMC. A larger via pad may improve manufacturing margins, but it introduces parasitic capacitance that can degrade high-speed channels. Reducing the layer count may lower raw PCB fabrication costs, but it can complicate return paths, impedance control, or the PDN. The correct trade-off depends on functionality, operating frequency, production volume, risk profile, and required operating life.
Begin with the Stackup and Real Manufacturer Tolerances
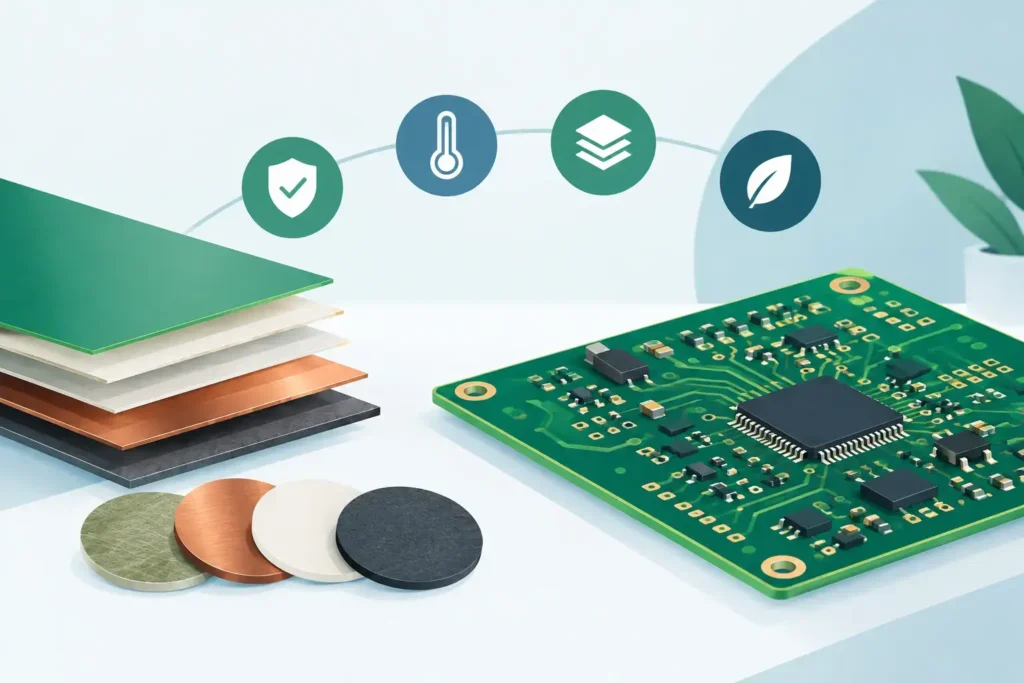
The stackup is one of the earliest and most critical DFM decisions. The layer build-up dictates more than just the single-ended and differential pair impedances. It influences aspect ratios, lamination quality, copper distribution, warpage, HDI sequencing, EMC performance, and available routing channels.
Therefore, a stackup must never rely on nominal dielectric thicknesses derived from an outdated reference project. Materials vary, copper foil exhibits tolerances, and prepreg flows during lamination. When a 100-ohm differential pair is critical, trace width and spacing must be calculated using a verified stackup from the selected fabricator—accounting for finished copper thickness after plating and realistic process tolerances.
On high-density multilayer boards, it is equally important to evaluate whether sequential lamination and microvias are required. While HDI often resolves BGA escape routing and shortens interconnects, it introduces additional process steps, increases cost, and tightens design rule constraints. Blind and buried vias should be implemented to solve specific electrical or mechanical constraints, not simply because the technology is available.
Copper balance must be evaluated across the entire panel. Large, asymmetric copper areas increase the risk of board warpage, misregistration, and thermal variation during reflow. Incorporating local copper thieving or adjusting plane geometry may be necessary, but any modifications must always be balanced against return paths, thermal dissipation, and EMC.
Routing Must Be Solderable, Inspectable, and Testable
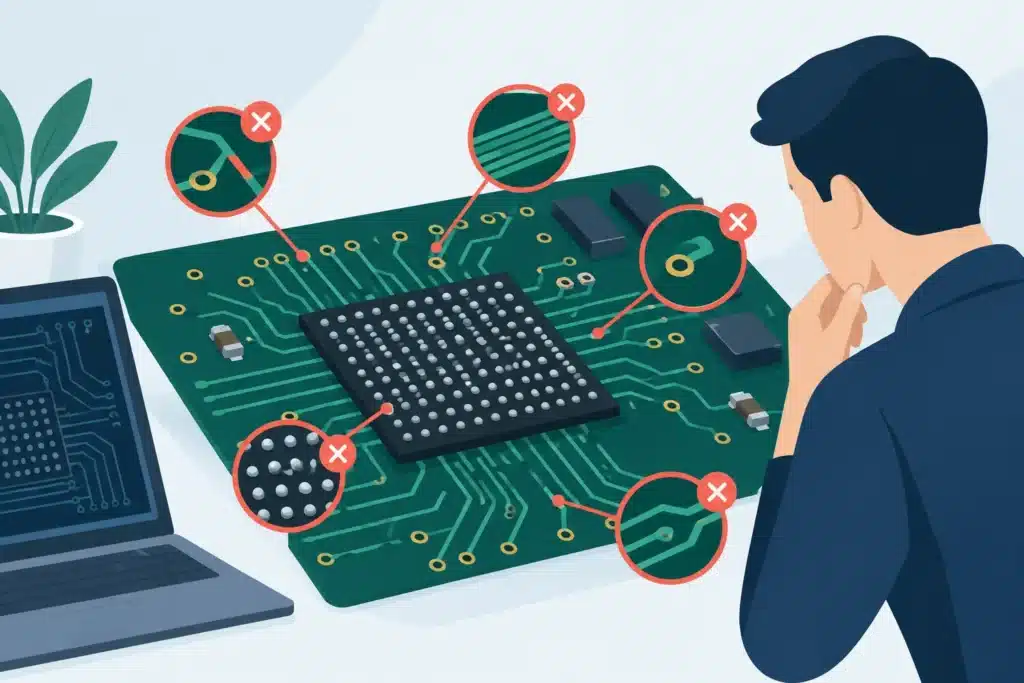
A densely packed layout may appear spatially efficient, but assembly yield depends on far more than board area. Component clearances must accommodate solder paste stencils, pick-and-place tooling, AOI, X-ray inspection, and potential rework. Optical and physical access become critical constraints, particularly around BGAs, QFNs, connectors, and tall components.
Fine-pitch components demand precise land patterns and solder mask definitions. Solder mask slivers that fall below the fabricator's process capabilities can detach during production, causing solder bridges. Via-in-pad technology may be required beneath BGAs; however, open vias will wick solder away from the pad. The standard solution is filled and capped vias, which must be explicitly specified and budgeted from the outset.
Thermal relief design is another area where standard CAD rules are frequently applied without sufficient analysis. Overly aggressive thermal reliefs ensure large copper planes are solderable, but they simultaneously restrict current-carrying capacity and thermal heat sinking. Direct connections may be required for power components and ground returns, yet they might necessitate selective soldering or a tailored reflow profile. There is no single universal rule for all pads.
Testability is an integral manufacturing discipline. Without physical access to relevant nets, fault isolation on prototype builds and production runs becomes slow and cost-prohibitive. Test points must be defined before available space is consumed by components and mechanical enclosures. Where physical probe access is unfeasible, boundary scan, built-in self-test (BIST), or functional testing should be incorporated as deliberate architectural choices.
Documentation Is an Integral Part of the Product
Manufacturing files are not merely an export from the layout tool. They represent the definitive technical specification of what the fabricator and EMS partner must build. Ambiguous notes, conflicting layer data, or omitted requirements force the vendor to make assumptions—and assumptions are an unacceptable control method in mission-critical electronics.
At a minimum, a comprehensive release package must include:
- PCB fabrication data with explicit layer definitions, board outline, cutouts, routing contours, and controlled impedance callouts.
- Stackup details, material specifications, copper weights, surface finish, IPC class, and applicable acceptance criteria.
- Drill files detailing tolerances, requirements for filled, capped, or tented vias, along with backdrill specifications if applicable.
- Assembly data including BOM, pick-and-place files, centroid definitions, component polarity, assembly drawings, and special soldering instructions.
- Test requirements, programming workflows, serialization protocols, and critical measurement point definitions.
Maintaining strict revision control is equally essential. The BOM, schematic, layout database, fabrication files, and mechanical models must all reference the identical release state. Otherwise, an accurately fabricated PCB may be populated using an obsolete component list or an incorrect placement file. Such discrepancies rarely stem from vendor error, but rather from deficient configuration management.
The DFM Review Must Occur Prior to Release
An effective DFM review evaluates the design against a specific fabrication facility and assembly process. It typically begins with design rule checks and manufacturing minimums, but it must extend to areas automated checks cannot interpret: critical component placement, solder paste volume, panel utilization, mechanical tolerances, thermal zones, test access, and stringent EMC or high-speed constraints.
For high-speed designs, the review must also verify that manufacturing-driven modifications do not compromise channel integrity. Stubs on through-hole vias, reference plane discontinuities, asymmetric differential pairs, and inadequate via fencing can all degrade operating margins. In RF designs, minor variations in solder mask, surface finish, or copper geometry can significantly shift impedance and resonance points.
Consequently, fabricator feedback must be evaluated from a technical perspective, not merely administratively. A suggested adjustment toward larger annular rings or wider clearances is often structurally sound, but it must be assessed against routing density, impedance, and circuit performance. The same applies to proposals for altering surface finishes, panel orientation, or layer configurations to reduce unit cost. A lower piece price is not a true cost saving if it compromises yield or introduces field failures.
Wise Choice Support treats these trade-offs as an integrated facet of the PCB layout process: electrical margins, manufacturing capabilities, and technical documentation are evaluated holistically prior to design release. This approach is critical in IPC Class 2 and Class 3 projects, where late-stage engineering changes can jeopardize qualification, delivery schedules, and traceability.
Integrate DFM Early into the Project Lifecycle
The most expensive manufacturing failures rarely occur because DFM rules were unknown. They occur because critical architectural decisions were deferred: the fabricator was selected too late, mechanical constraints shifted after routing, components were placed without a test strategy, or the stackup was finalized without electrical modeling.
The practical solution is to validate the manufacturing pathway while the layout remains mutable. Establish the technology baseline, anticipated production volumes, IPC classification, component procurement strategy, and test methodology early. Subsequently, execute a structured review of the stackup, critical routing, land patterns, assembly accessibility, and final release data prior to initial fabrication.
A production-ready PCB is not a layout that can merely pass through fabrication. It is a design where essential tolerances are accounted for, critical engineering compromises are made deliberately, and manufacturing operates from definitive, unambiguous data. This discipline ensures shorter NPI cycles and highly reliable hardware once the board leaves the laboratory.